
@hwaqseo
- Followers 0
- Following 0
- Updates 396
Blog
The Architects of the Flawless Canvas
Liquid foundation manufacturers operate at the sophisticated nexus of cosmetic chemistry, dermatology, and color science, dedicated to producing the complex emulsions that serve as the base for millions of makeup routines worldwide. Their core challenge is to formulate a product that is both a cosmetic and a quasi-skincare item—a pigmented fluid that must evenly mask imperfections, match living skin tones, feel comfortable for all-day wear, and interact harmoniously with a wide variety of skin types and conditions. This requires a deep mastery of emulsion technology, pigment dispersion, and stabilizing chemistry to create a product that won't separate, oxidize, or cause irritation, delivering a consistent experience from the first drop to the last.
The Science of the Base: Emulsion Engineering
At its heart, liquid foundation is an oil-in-water (O/W) or water-in-oil (W/O) emulsion, or increasingly, a silicone-based system. The choice of base dictates the final feel and performance. O/W emulsions (lighter, more hydrating) are created by dispersing oil droplets within a continuous water phase using emulsifiers like cetyl alcohol or glyceryl stearate. W/O emulsions (more water-resistant, richer) trap water droplets in oil, often using emulsifiers like sorbitan sesquioleate. Silicone-based foundations use volatile silicones (like cyclomethicone) for an initial smooth, dry-touch application that evaporates, leaving pigments and conditioning agents on the skin. The manufacturing process begins with creating a stable pre-mix of the water and oil phases separately, heating them to dissolve ingredients, and then combining them under high-shear homogenization to form micro-droplets for a stable, smooth emulsion.
The Art of Color: Pigment Dispersion and Shade Matching
The true technical prowess lies in color incorporation and stability. Manufacturers use inorganic pigments (iron oxides for red, yellow, black) and organic lakes for vibrancy. These hydrophobic pigments must be perfectly wetted, de-agglomerated, and dispersed into the emulsion. This is achieved through roller milling or high-pressure homogenization, which breaks down particle clusters to sub-micron levels, preventing a gritty feel and ensuring even color distribution. Shade matching is a precise science involving spectrophotometers and standardized lighting booths. Manufacturers maintain extensive shade libraries and use computer-aided formulation to create bases with specific undertones (pink, yellow, neutral, olive) and adjust for oxidation—a chemical reaction where foundation darkens upon contact with air and skin oils, which must be predicted and corrected for in the lab.
The Production Line: From Vat to Vial
Scale production is a controlled, sequential process. Large batches are made in stainless steel jacketed kettles with temperature and shear controls. After the base emulsion is formed and cooled, the pre-dispersed pigment paste is incorporated under gentle mixing to avoid introducing air. Active ingredients (like hyaluronic acid, vitamins, SPF filters) are added last, at lower temperatures, to preserve their efficacy. The final product undergoes de-aeration to remove bubbles before filling. Filling occurs in a cleanroom environment to ensure microbiological integrity. Product is dispensed into bottles, which are then fitted with pumps, droppers, or caps. The entire line must be calibrated for the specific viscosity of the formula, from thick creams to runny serums.
The Engine of Creation in Workshops Worldwide
A power drill factory is a highly specialized manufacturing hub dedicated to producing one of the most fundamental and versatile tools in construction, manufacturing, and DIY. This facility is where the abstract concept of rotational force is translated into a mass-produced, handheld device capable of boring holes, driving fasteners, and mixing materials. The factory’s operations encompass a broad spectrum of engineering disciplines, from designing high-efficiency electric motors and durable mechanical transmissions to integrating advanced electronics for battery management and user control. Its output powers everything from home furniture assembly to the construction of skyscrapers, making it a cornerstone of modern productive capacity.
Product Line Specialization: From Subtle to Savage
While called a "drill factory," such a facility typically manufactures a family of related rotary tools. The core product is the standard drill driver, a versatile tool for drilling and light fastening. A separate, more robust line produces hammer drills, which incorporate a pneumatic or mechanical impact mechanism alongside rotation to tackle masonry. Another critical line is dedicated to impact drivers, which deliver high rotational torque through concussive internal strikes (anvils and hammers), making them ideal for driving long screws and bolts. High-end factories also produce right-angle drills and rotary hammer drills for specialized trades. Each type requires distinct internal mechanisms, though they share common components like motors, chucks, and housings, allowing for some modularity in production.
Core Component Manufacturing: The Heart of the Drill
The manufacturing process is segmented by core assemblies. The motor—either a brushed DC motor for cost-sensitive models or a brushless DC (BLDC) motor for premium cordless tools—is produced on a dedicated line involving winding copper coils, assembling magnets and armatures, and balancing rotors. The gearbox and transmission are precision assemblies. Planetary gear sets, machined from hardened steel, are housed in aluminum or magnesium gear cases. For hammer drills, an intricate impact mechanism (either a mechanical clutch system or a pneumatic piston) is manufactured and tested separately. The keyless chuck, a marvel of self-centering mechanics, is often sourced from specialized suppliers but assembled onto the spindle in-house. These sub-assemblies converge on the main assembly line.
The Assembly Line: Convergence of Mechanics and Electronics
The main assembly line is a carefully choreographed sequence. It begins with the clamshell housing (often high-impact polymer or metal), into which the motor is installed. The gearbox is then mounted to the motor output shaft. For cordless tools, the electronic controller board, which governs speed, torque, and battery communication, is installed and connected. The switch, trigger (with variable speed control), and forward/reverse selector are fitted. The chuck is mounted and secured to the output spindle. Finally, for cordless models, the battery interface is installed. A parallel line assembles lithium-ion battery packs, involving spot-welding cells together, installing a Battery Management System (BMS) board, and encapsulating them in a robust plastic casing.
The Exposed Heartbeat of High-Torque Performance
The side-hanging gear motor electric scooter represents a distinct and purpose-driven architectural choice in the world of electric two-wheelers, diverging from the dominant hub-motor paradigm. This design features a compact, high-RPM electric motor mounted externally on one side of the scooter's rear wheel, connected via a reduction gearbox and a final drive chain or belt. This configuration is not merely a stylistic quirk; it is a deliberate engineering solution that prioritizes high torque output, thermal management, and serviceability over the seamless integration and lower maintenance of a hub motor. It appeals to riders and manufacturers seeking robust performance, particularly in demanding conditions like steep hills, off-road use, or for carrying heavy loads, where its mechanical advantages become pronounced.
The Mechanics of Decentralized Power
The core principle involves separating the motor from the wheel hub. A small, lightweight brushless DC (BLDC) motor spins at very high speeds (often 3,000 RPM or more). This rotational power is fed into a multi-stage planetary or spur gear reduction box attached directly to the motor casing. The gearbox, with a reduction ratio typically between 1:4 to 1:10, drastically increases torque while reducing the output shaft speed to a usable level. This output shaft then drives the rear wheel via a final drive chain or a toothed synchronous belt. This separation allows each component to be optimized: the motor can be small and spin fast for power density, the gearbox can be designed for specific torque multiplication, and the wheel remains a simple, strong, and lightweight component. The side-mounting provides excellent natural air cooling for both the motor and gearbox, preventing thermal throttling during sustained high-load use.
Performance Profile: Torque and Thermal Advantages
The primary benefit is superior torque delivery, especially at low speeds. The gear reduction multiplies the motor's torque significantly, allowing the scooter to accelerate briskly from a standstill and climb steep gradients that would stall or overheat a similarly powered hub motor. The external mounting provides exceptional thermal dissipation. Hub motors, encased within the wheel, can struggle to shed heat, leading to efficiency drops and potential damage under continuous load. The side-hanging motor's exposed fins and airflow act as a natural heatsink, sustaining performance over longer, harder rides. This makes the design particularly favored for performance-oriented, off-road, or cargo scooter applications where sustained power is more critical than urban elegance.
Handling, Maintenance, and Practical Trade-offs
This configuration introduces specific dynamics. The unsprung weight is reduced compared to a hub motor (as the heavy motor is part of the frame, not the wheel), which can, in theory, improve suspension response and wheel control over rough surfaces. However, the lateral weight bias from the side mount can be felt during very low-speed maneuvers or when lifting the scooter. The exposed mechanical parts (chain/belt, gearbox) require regular maintenance—lubrication, tension adjustment, and protection from grit—unlike the "sealed for life" aspect of a hub motor. They are also more vulnerable to impact from curbs or debris. Conversely, this exposure makes repairs and upgrades vastly simpler; the motor, gearbox, or drive system can be serviced or replaced individually without dismantling the wheel hub.
The Cornerstone of Controlled Flow
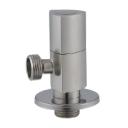
Angle valve manufacturing is the specialized industrial process of producing compact quarter-turn or multi-turn valves where the inlet and outlet ports are oriented at a 90-degree angle. These ubiquitous fittings, essential for isolating or regulating flow in tight spaces behind toilets, under sinks, and within industrial panels, require a blend of metallurgy, precision machining, and rigorous assembly to ensure leak-free operation over thousands of cycles. The manufacturing journey transforms raw metal castings or forgings into durable, reliable components that must seamlessly integrate with global plumbing and piping standards, balancing cost-efficiency with unwavering performance in both residential and demanding commercial environments.
From Raw Material to Rough Form: Casting and Forging
The process begins with creating the valve body, the primary pressure-containing component. For brass valves—the most common type—hot forging or sand casting are predominant methods. Hot forging involves heating brass billets and stamping them into a near-net-shape under immense pressure in closed dies. This produces a grain structure that follows the body's contours, resulting in superior strength, density, and pressure resistance, ideal for higher-grade valves. Sand casting is a more cost-effective method for complex shapes or lower volumes, where molten brass is poured into sand molds. The rough castings or forgings are then cleaned via tumbling or shot blasting to remove scale and burrs before moving to precision machining.
Precision Machining: Creating the Functional Geometry
This stage is where the rough body becomes a functional valve. CNC (Computer Numerical Control) machining centers perform a series of critical operations with micron-level accuracy. First, facing and boring machines create the flat sealing surfaces and precise internal cavities for the valve seat. Next, threading operations cut the inlet and outlet threads—typically ISO 7-1 (Rp) parallel threads or NPT tapered threads—ensuring they meet exact pitch and diameter standards for a perfect seal with pipe fittings. Simultaneously, the bonnet thread and stem guide are machined to allow the stem to move smoothly. Separate lines produce other components: the stem is turned and threaded from brass or stainless steel rod; the handle is die-cast; and the critical sealing elements—the washer/seal (often EPDM or PTFE) and the ceramic disc cartridge for quarter-turn models—are sourced or produced in-house.
Assembly, Finishing, and the Leap to Automation
The assembly line brings all components together. For traditional compression-style angle valves, a worker or automated cell inserts the seat, places the stem with its attached washer into the body, screws on the bonnet (often with a packing seal), and attaches the handle. For modern ceramic disc cartridge valves, the precision-molded ceramic plates are inserted into a cartridge, which is then pressed or screwed into the body—a design that offers longer life and drip-free operation. After assembly, valves undergo surface finishing. Electroplating (typically nickel-chromium) in multi-stage baths provides corrosion resistance and a shiny, easy-clean finish. Polishing may precede plating for a premium look. Automated lines have revolutionized this process, with robotic arms moving parts between stations, performing laser engraving of logos/specs, and conducting initial functional tests.
Manufacturing Mindfulness: The Hub of Sensory Tool Production
A bubble blowing decompression toys factory operates at the intersection of polymer science, precision manufacturing, and wellness-centric product design. This specialized facility is dedicated to mass-producing the popular sensory toys known for their satisfying cycle of pressing to form a bubble and popping it back. The factory’s core competency is not just molding silicone, but mastering the precise material formulations and manufacturing tolerances required to create that perfect, reliable tactile feedback—a soft yet resistant squish, a smooth bubble formation, and a durable membrane that withstands thousands of cycles. It transforms raw elastomers into tools that serve markets ranging from mainstream retail and promotional giveaways to therapeutic supply for education and occupational health.
Material Science: Formulating the Perfect Feel
The entire product experience hinges on the material. Leading factories use platinum-cure liquid silicone rubber (LSR) or high-grade Thermoplastic Elastomers (TPE). LSR is preferred for premium toys due to its exceptional durability, purity (free of phthalates and BPA), excellent tear strength, and consistent performance across temperature ranges. The factory’s chemical engineers work with base polymers and catalysts, adjusting the Shore hardness (typically between A10 to A30 for a soft, squeezable feel) and elastic recovery speed. The formulation must achieve a delicate balance: be soft enough to invert easily, yet strong enough to resist puncturing; have a high tear strength to prevent failure at the thin membrane, and maintain its properties without becoming sticky or degrading over time. This proprietary mix is the factory’s foundational intellectual property.
Precision Molding: The Art of the Thin Wall
The manufacturing challenge lies in creating a seamless, hollow object with a wall thickness that varies strategically—thicker at the base for structure, dramatically thinner at the dome’s apex to form the bubble. This is achieved through injection molding using high-precision, temperature-controlled molds. For LSR, a liquid silicone injection molding (LSR IM) machine is used. The two-part mold is designed with calculated injection points and venting to allow the viscous liquid silicone to fill the cavity completely and cure uniformly without air traps. The mold itself is machined from polished tool steel to a mirror finish, as any imperfection would be replicated on the toy’s surface, affecting feel and bubble formation. The cycle time, temperature, and pressure are tightly controlled to ensure every unit is identical. After demolding, toys often go through a post-curing oven to fully stabilize the silicone’s properties.
Quality Assurance: Testing for Endless Satisfaction
Given that the product’s value is in repetitive use, quality control is rigorous and focused on longevity and safety. Destructive and non-destructive testing are both employed. Sample toys from each batch undergo automated cycle testing, where a machine presses and releases the bubble thousands of times to simulate extended use and verify the membrane’s fatigue resistance. Material safety certification is mandatory; batches are tested by accredited labs for heavy metals, migration of substances, and compliance with standards like EN-71 (Europe), ASTM F963 (U.S.), and CPSIA. Visual and tactile inspection ensures there are no flash (excess material), bubbles, or inconsistent texture. The factory’s reputation depends on delivering toys that perform consistently and safely from the first press to the thousandth.
Customization, Scalability, and Market Agility
A successful factory offers more than a generic product line. It provides custom molding services (OEM/ODM) for clients wanting unique shapes—brand logos, custom animals, or thematic designs. This involves designing and machining new molds, a significant upfront investment that demonstrates the factory’s capability. They manage production scalability, from small runs of specialized therapeutic tools to massive orders for global retail chains. Packaging is also critical; toys are often individually sealed in poly bags or placed in form-fitting plastic clamshells to protect the sensitive silicone surface from dust and damage during logistics. By combining material expertise with flexible manufacturing, the factory caters to diverse channels, from online fidget toy stores to corporate stress-relief promotional campaigns.
Reimagining the Rotating Heart of Lubrication
The oil pump-carbon fiber plastic-drive shaft represents a paradigm shift in the design of a fundamental engine component, moving from a traditional machined steel part to an advanced engineered composite. This shaft is the critical link that transmits rotational drive—typically from the crankshaft or camshaft—to the pump's internal gerotor or gear set, thereby pressurizing the engine's lubrication system. Re-engineering it from carbon fiber-reinforced polymer (CFRP) targets a multifaceted performance gain: achieving dramatic weight reduction to improve engine responsiveness and efficiency, leveraging the material's high damping properties to reduce noise and vibration, and utilizing net-shape manufacturing to integrate complex features. This innovation speaks to the pursuit of holistic efficiency in next-generation powertrains.
The Composite Advantage: Beyond Weight Savings
While weight reduction is a primary driver, the benefits of CFRP are more profound. The high specific strength and stiffness of the material allow the shaft to handle significant torsional and bending loads with a fraction of the mass of steel, reducing rotational inertia. This directly translates to improved engine throttle response and lower parasitic loss. Crucially, CFRP's inherent damping characteristics absorb high-frequency vibrations from the engine and pump, contributing to a quieter overall engine sound profile and reducing stress on adjacent components. Furthermore, advanced thermoset or thermoplastic matrices can be formulated for excellent chemical resistance to modern engine oils and dimensional stability across a wide temperature range (-40°C to 150°C+), ensuring reliable operation throughout the engine's lifecycle.
Engineering for Torque and Interface Integrity
The central design challenge is ensuring reliable torque transmission and longevity at the shaft's interfaces. The spline or keyway that mates with the driving component must be engineered to withstand shear forces without wear or deformation. This is often addressed by localized metallic reinforcement—integrating a metal sleeve or insert into the composite during molding, or using advanced 3D woven preforms that orient fibers optimally to handle torsional stress. Similarly, the journal surfaces that rotate within bushings or bearings may incorporate wear-resistant polymer sleeves or be treated with a specialized coating. The shaft's geometry is also optimized using Finite Element Analysis (FEA) to manage stress concentrations, prevent critical-speed resonances, and ensure the pump's internal gears remain in perfect alignment under all operating conditions.
Manufacturing Precision for a Dynamic Component
Manufacturing such a performance-critical part requires advanced composite processes. Resin Transfer Molding (RTM) or compression molding of pre-impregnated carbon fiber sheets (prepreg) is common for high-volume, net-shape production. These processes allow precise control over fiber layup and orientation to tailor strength and stiffness directionally. For the highest performance, filament winding of carbon fiber onto a mandrel may be used to create a hollow shaft with an exceptional torsional strength-to-weight ratio. The molding tooling itself is engineered to form the complex spline geometry and any integrated features in a single shot, eliminating secondary machining. Every shaft undergoes rigorous non-destructive testing (NDT) like ultrasound to check for voids or delamination, and is balanced to prevent vibration.
In warehouses and industrial facilities, Scattered Tools can disrupt workflow and complicate maintenance operations. With large spaces and multiple workstations, tools may be left behind after tasks are completed, leading to inefficiencies and challenges in daily management. Establishing structured tool management systems is essential for smooth operations.
Scattered tools make it harder for teams to maintain consistent work rhythms. When tools are not returned to designated locations, other workers may struggle to find what they need, leading to downtime. Visual storage systems, such as shadow boards and labeled racks, provide clear guidance on where each tool belongs and help maintain order.
Inventory control is another concern. Scattered tools increase the risk of loss, misplacement, and duplication of purchases. Without clear tracking, facilities may spend more on replacements than necessary. Simple sign-out procedures and periodic audits help maintain better oversight of tool usage and availability.
From a safety standpoint, scattered tools can obstruct pathways and emergency exits. Items left on the floor or near machinery can interfere with movement and increase the risk of incidents. Clear storage zones and regular inspections help reduce these risks and support safer working conditions.
By improving the management of scattered tools, warehouses and industrial facilities can create more organized environments. Structured storage, visual cues, and routine checks contribute to higher operational efficiency and a safer workspace for all personnel.
Decoding the Cost Drivers of Mold Complexity
The side core pulling price is a significant variable in injection mold costing, representing the investment required to form features that are not in the main opening direction of the mold. This cost is not a simple line item but a composite of design engineering, precision machining, and assembly of specialized mechanisms that must operate reliably for hundreds of thousands of cycles. Accurately estimating this figure requires analyzing the geometric challenge of the undercut, the chosen technical solution, and the performance demands of the production run. Ultimately, this price reflects the premium paid to achieve complex part geometries that would otherwise be un-moldable.
The Core Cost Components: Mechanism and Manufacture
The price breaks down into several key areas. The most fundamental is the type of actuation system. A mechanical cam (angled pin) system is generally less expensive upfront. Its cost lies in the precision machining of the cam, the wear plates, and the core slider itself. However, its price increases with the complexity of the motion (longer travel, tighter angles) and the need for higher durability. A hydraulic cylinder system carries a higher base price due to the cylinder unit, hydraulic manifolds, and more complex mold plumbing. However, for long strokes or complex sequences, it can be more cost-effective than an oversized mechanical system. The second major component is machining and materials. The core block, slider, guides, and wear plates require significant CNC machining time. Using pre-hardened or hardened tool steel (like H13) instead of mild steel increases material cost but is essential for longevity, impacting the price.
The Multipliers of Complexity and Integration
Beyond the base mechanism, multiple factors act as cost multipliers. The number of side actions is direct: two independent side cores cost significantly more than one. Core geometry is critical; a simple rectangular core is cheaper to machine than one with complex contours or multiple sealing faces. Integration requirements add substantial cost: incorporating conformal cooling channels into the side core for better cycle times, adding position sensors for mold safety, or designing lifter systems that combine side and upward motion all increase engineering and machining complexity. Furthermore, if the side action operates in a hot runner manifold zone, the design becomes more intricate to avoid interference, requiring careful thermal management and possibly customized components, driving the price higher.
The Trade-Offs: Standardization, Design, and Total Cost of Ownership
Molders can manage costs through strategic choices. Utilizing standardized catalog components for sliders, guides, and cylinders from suppliers like HASCO or DME can reduce cost and lead time compared to fully custom parts. The most profound cost control occurs during the design for manufacturability (DFM) phase. Simplifying the undercut, minimizing the required core travel, or redesigning the part to eliminate a side action altogether are the most effective ways to reduce the side core pulling price. It's also crucial to consider the total cost of ownership. A cheaper, lower-quality system may lead to frequent maintenance, downtime, and premature failure during production, far outweighing the initial savings. Investing in robustness is often more economical for high-volume production.