
@hwaqseo
- Followers 0
- Following 0
- Updates 384
Category: ABS Luggage

Core Product Definition
A construction machinery starter is a high-torque electric motor designed to crank large-displacement diesel engines in heavy equipment including excavators, bulldozers, loaders, cranes, and graders. This critical component engages with the engine flywheel to initiate combustion, transforming electrical energy from the battery into mechanical rotation powerful enough to overcome the high compression ratios of diesel engines. Unlike automotive starters, construction machinery starters are engineered for extreme durability, delivering reliable performance in dusty construction sites, cold climates, and continuous operation environments.
Fundamental Operating Principle
The construction machinery starter operates through electromagnetic engagement and high-torque motor rotation. When the operator turns the ignition key, current flows to the solenoid, which simultaneously closes the main electrical circuit and pushes the pinion gear forward to mesh with the engine flywheel ring gear. The electric motor then rotates, transferring torque through the pinion to crank the engine. Once the engine starts and exceeds starter speed, an overrunning clutch disengages the pinion to prevent damage from overspeeding. This sequence must occur reliably thousands of times throughout the equipment's service life.
12-Volt Versus 24-Volt Systems
Construction machinery starters are available in two primary voltage configurations tailored to different equipment sizes. Twelve-volt starters are designed for smaller or medium-sized construction equipment including compact excavators, wheel loaders, and auxiliary machinery with four to six cylinder diesel engines . These systems draw power from standard electrical configurations and offer cost-effective reliable performance in moderate conditions . Twenty-four volt starters operate on dual-battery systems delivering higher starting torque for large diesel engines found in heavy-duty excavators, mining trucks, and cranes . These systems provide improved reliability in cold climates and better voltage stability under load, making them standard in most heavy construction machinery .
Gear Reduction Technology
Advanced construction machinery starters utilize internal gear reduction systems to multiply torque output while using smaller, more efficient motors. A planetary gear train between the motor armature and the pinion drive increases rotational force by three to four times compared to direct-drive designs . This allows the starter to draw less current from the battery while delivering higher cranking torque essential for cold starts and high-compression diesel engines . The gear reduction mechanism also enables more compact starter packaging, accommodating space-constrained engine compartments in modern machinery. Gear reduction starters typically achieve up to thirty percent higher torque output than conventional designs .
Direct Gear Reduction Starters
Direct gear reduction construction machinery starters use a compact gear train to amplify torque while drawing less current from the battery. These starters are ideal for smaller engines and offer excellent cold-weather starting performance combined with improved energy efficiency . Their lightweight, compact design makes them suitable for machines where space and weight are critical considerations . However, they may be less suitable for very large engines requiring maximum torque capacity .
Permanent Magnet Starters
Permanent magnet construction machinery starters utilize high-strength magnets instead of traditional field coils to generate the magnetic field for motor rotation. This design eliminates heavy copper windings, resulting in lighter, more compact units with improved efficiency and faster response times . The permanent magnet configuration reduces power loss and enables quick engagement ideal for mid-sized excavators, telehandlers, and machines where installation space is limited . These starters must be carefully managed to prevent magnet degradation under excessive heat conditions .
Pre-engaged Starters
Pre-engaged construction machinery starters use a solenoid to move the pinion gear into engagement with the flywheel before the motor spins. This prevents gear clash and ensures smooth, quiet engagement critical for heavy-duty engines . The design reduces wear on flywheel teeth and provides high reliability under continuous load conditions . These starters are larger and heavier than some alternatives but offer superior durability for large-engine applications in industrial environments.

Core Business Definition
A bearing puller manufacturer is a specialized industrial company that designs and produces mechanical tools for removing bearings, gears, pulleys, and other press-fit components from shafts without causing damage. These manufacturers engineer pullers in various configurations including two-jaw, three-jaw, internal pullers, slide hammer pullers, and hydraulic pullers for heavy-duty applications. The manufacturing process combines metallurgy, precision machining, heat treatment, and assembly operations to create tools that apply controlled force for maintenance and repair across automotive, industrial, aerospace, and agricultural sectors.
Major Manufacturing Facilities and Global Presence
Bearing puller manufacturers operate across multiple continents with specialized expertise. KUKKO, founded in Germany on October 1, 1919, by Alfred Kleinbongartz and Emil Kaiser, has operated as a globally active family business for over one hundred years through four generations, selling products in more than one hundred countries worldwide . Headquartered in Hilden, Germany, KUKKO maintains manufacturing operations with stringent quality control and has established offices in Poland, the Netherlands, Italy, and the United States . Their product range includes one hundred fifty puller types and five hundred insert sizes, specializing in non-destructive disassembly of gears, bearings, and ball bearings .
In China, Dongning Tools (Ningbo) Co., Ltd, operating as DNT Tools, has manufactured hand tools, mechanical tools, and automotive tools since 1999, producing bearing pullers, bearing separators, gear pullers, and wheel bearing removal tools for workshops and garages worldwide . Tianda Tools in Zhangjiagang City, Jiangsu Province, manufactures gear pullers and related tools with annual production capacity reaching one million pullers, exporting over sixty percent of products to Europe and the United States . Taizhou Yindu Tools Co., Ltd., located in Zhejiang Province, produces hydraulic bearing pullers ranging from five to fifty ton capacity for car maintenance factories, machine shops, and repair facilities .
India hosts established manufacturers including Ludhra Overseas, operating since 1952 in Jalandhar, Punjab, manufacturing two-leg bearing pullers from drop forged carbon steel, hardened and tempered, available in chrome plated or auto black finishes, exporting to more than ten countries worldwide . Tools Corporation Ltd in Faridabad, Haryana, manufactures Jhalani brand bearing pullers for the Indian market .
Product Types and Configurations
Bearing puller manufacturers produce various puller types each engineered for specific applications and access situations. External pullers grip components from the outside, using two or three jaws to grasp gears, belt pulleys, or ball bearings accessible on shafts, applying force through mechanical or hydraulic spindles to release them . Internal pullers remove bearings and bushings not accessible from the outside because they sit in recesses or housings, requiring countersupports or sliding hammers to extract them . Mechanical pullers utilize threaded spindles generating force through leverage, available in fixed jaw or adjustable configurations. Hydraulic pullers incorporate hydraulic cylinders to generate high pulling forces, with models available from five to fifty tons capacity for demanding industrial applications . Bearing separator pullers use sharp, wedge-shaped cutting edges positioned under parts to pull off or separate components using specialized pulling devices .
Manufacturing Processes and Materials
Production within a bearing puller manufacturer involves multiple precision operations using high-quality materials. Jaws and bodies are typically drop forged from carbon steel or chrome vanadium alloy steel, creating grain structures optimized for strength and durability . Forged components undergo machining operations including CNC turning, milling, and drilling to produce precise thread forms on forcing screws and accurate jaw geometries ensuring proper gripping. Heat treatment processes including hardening and tempering achieve optimal hardness balancing wear resistance with toughness to prevent brittle failure under load . Surface finishing through chrome plating, zinc plating, or auto black coatings provides corrosion resistance and professional appearance. Assembly operations integrate jaws, screws, and frames into complete tools ready for packaging.
Specialized Puller Technologies
Advanced bearing puller manufacturers develop innovative solutions for challenging applications. PULLPO technology enables contact-free dismantling of ball bearings where neither the puller nor spindle contacts the shaft or housing.

Core Business Definition
An optical eyewear factory is a specialized manufacturing facility that produces prescription glasses, sunglasses, reading glasses, and related vision correction products. These factories integrate frame production, lens manufacturing, and final assembly operations to create complete eyewear products meeting international quality standards. The manufacturing process combines precision engineering, materials science, and optical technology to produce eyewear that corrects vision while providing comfort, durability, and aesthetic appeal. Factories range from large-scale facilities producing millions of units annually to specialized operations focusing on premium handmade frames or advanced lens technologies.
Global Manufacturing Landscape
Optical eyewear factories are concentrated in key regions with established optical industries serving international markets. Wenzhou, Zhejiang province, hosts numerous manufacturers, including Wenzhou Rainbow Optical, founded in 2001, specializing in optical frames, sunglasses, and reading glasses with established markets across Europe, North America, and the Middle East . Mike Optical, established in Wenzhou in 2010, operates additional branches in Jiangsu Danyang and Hangzhou, employing roughly 200 worker,s including more than 20 professional eyewear designers with strong research and development capabilities. Danyang, Jiangsu province, serves as a major optical hub where companies like Danyang Mike Optical maintain production bases. Emerging manufacturing centers include India, where Lenskart has broken ground on a 50-acre integrated facility in Hyderabad, representing an investment of 1,500 crore rupees, expected to eventually manufacture over 200,000 glasses per day, serving domestic, Asian, and Middle Eastern markets.
Manufacturing Facilities and Scale
Leading optical eyewear factories operate substantial production facilities with advanced capabilities. Sunpet Industries, established in 1972, operates a factory complex in China spanning 30,000 square meters across six blocks, housing approximately 600 workers with ISO9001 quality management and ISO14001 environmental certification. In 1994, Sunpet became the first to establish an ultra-precision machining centre for aspherical plastic lens manufacturing in Hong Kong, subsequently installing additional advanced ultra-precision machines. New facilities continue development, such as the Dexi Optical in Sichuan province, a 10-story modern factory spanning nearly 10 acres, designed to collaborate with Zeiss, Essilor, and other international brands, with annual production capacity exceeding 200,000 optical products.
Lens Manufacturing Technology
The heart of optical eyewears factory operations lies in precision lens fabrication. Premium manufacturers like Zeiss utilize advanced free-form technology, where semi-finished lens blanks with pre-formed front surfaces are processed using 5-axis CNC methods, completing lens generation in approximately 90 seconds through three distinct steps: grinding, shaping, and precision surfacing using natural diamond tools controlling tens of thousands of processing points . This technology enables creation of completely customized optical surfaces tailored to individual prescriptions and visual requirements .
Alternative manufacturing approaches include innovative fluidic shaping technology developed for low-resource settings, where liquid photopolymer is injected into elliptical frames submerged in immersion liquid of equal density, utilizing surface tension to form two lens surfaces corresponding to the required prescription . After several minutes of curing under low-power LED arrays, complete solid lenses are obtained requiring no post-processing, demonstrating potential for local manufacturing where conventional machining technologies remain inaccessible .
Frame Material Production
Optical eyewears factories produce frames from diverse materials each requiring specific manufacturing techniques. Acetate frames utilize cellulose-based sheets cut, shaped, and polished through multi-stage processes including CNC machining, tumble polishing, and extensive hand finishing. Metal frames including titanium, stainless steel, and monel are stamped, welded, and surface finished through electroplating and coating applications. TR90 and other injection-molded thermoplastic frames are produced through high-pressure molding creating lightweight, durable designs. Each material category requires specialized equipment and skilled operators to achieve consistent quality.
Core Business Definition
A PVC raincoat film factory is a specialized manufacturing facility that produces polyvinyl chloride films specifically engineered for rainwear and waterproof apparel applications. These factories transform raw PVC resin into flexible, durable films through calendering processes that create materials with precisely controlled thickness, texture, and performance characteristics. The resulting films serve as the primary material for raincoats, ponchos, children's rainwear, workwear, and various waterproof garments where protection from moisture is essential. Manufacturers range from large-scale operations producing hundreds of millions of yards annually to specialized facilities focusing on specific film types and applications.
Major Manufacturing Facilities
Several prominent PVC raincoat film factories operate globally with significant production capabilities. Baixing Group Co., Ltd., established in 1988, is one of the largest PVC manufacturers in mainland China with five branch factories producing different PVC products . Located in Lijia Town of Changzhou City, Jiangsu Province, they produce more than 500 million yards of PVC and PU coated fabrics annually alongside 60,000 tons of PVC films . These materials are ideal for producing outerwear and raincoats, with the company operating its own raincoat factory capable of supplying 250,000 pieces monthly using their raw materials .
Nantong Huaneng New Material Co., Ltd., founded in 2005 with nine calendering production lines, specializes in manufacturing PVC products including transparent film, color film, printing film, engineering film, and specifically raincoat film . Similarly, Jiangsu Juhuaneng New Material Technology Co., Ltd. operates nine advanced calendering lines producing PVC raincoat film alongside antistatic, colors, super clear, and crystal PVC films .
Calendering Manufacturing Process
The production of PVC raincoat film relies primarily on calendering technology, which achieves uniform thickness and consistent performance characteristics. The process begins with mixing PVC resin with plasticizers that determine the film's flexibility, stabilizers that prevent degradation from heat and UV exposure, and pigments for color. This compound is heated and passed through a series of heated rollers called a calender, which progressively reduce thickness while maintaining precise dimensional control. The calendering process ensures uniform thickness with tolerances as tight as plus or minus 0.02 millimeters, essential for consistent raincoat production . Linyang PVC operates four PVC calendering production lines and added a new wide-width rolling production line in 2015, which is currently the widest in the world .
Material Properties and Formulations
PVC raincoat film is formulated as soft or flexible PVC through the addition of plasticizers to the base PVC resin . Standard soft PVC films range from 0.125 millimeters to 3 millimeters in thickness, with raincoat applications typically using the thinner end of this spectrum for comfort and flexibility . The material is inherently waterproof, providing complete barrier protection against moisture. High-quality raincoat films achieve IPX6 waterproof ratings, blocking rain and moisture ingress effectively, with some advanced models offering UPF 50+ UV protection that blocks 98 percent of UV rays for outdoor worker safety .
Specialized Raincoat Film Grades
Different rainwear applications require specific film grades from PVC raincoat film factories. Base models with 0.2 to 0.25 millimeter thickness suit casual raincoats and lightweight accessories where cost efficiency matters. Advanced models with 0.25 to 0.35 millimeter thickness provide IPX5 waterproofing for industrial covers and moderate outdoor gear. Professional grade films from 0.35 to 0.4 millimeter thickness offer IPX6 waterproofing and UPF 50+ UV protection for demanding applications such as firefighter gear and extreme condition rainwear . Tensile strength can reach 19.5 MPa in professional grades, exceeding industry benchmarks by thirty percent for use in extreme conditions .
Surface Finishing and Customization
PVC raincoat film factories offer various surface finishing options to meet specific rainwear requirements. High-gloss finishes create the shiny appearance associated with traditional rainwear aesthetics. Matte finishes offer sophisticated, low-reflectivity surfaces for modern designs. Ribbed textures enhance durability and tear resistance while maintaining structural integrity in dynamic environments . Anti-UV coatings can be customized from UPF 30 to UPF 50 plus levels depending on environmental needs . Films can be produced in normal clear, super clear, color, and decorative varieties .
Core Business Definition
An acetate sunglasses factory is a specialized manufacturing facility that produces eyewear frames using cellulose acetate, a plant-based plastic derived from cotton fibers and wood pulp. Unlike injection-molded frames, acetate sunglasses are typically crafted from flat sheets or blocks of material through a multi-stage process involving cutting, machining, and extensive hand polishing. These factories range from large-scale producers with hundreds of workers to smaller artisanal workshops specializing in handmade frames, serving global brands, independent designers, and private label customers worldwide.
Major Manufacturing Hubs
Acetate sunglasses factory operations are concentrated in specific regions with established eyewear industries. Wenzhou, Zhejiang province hosts numerous manufacturers including Wenzhou Deco International, established in 2005, operating a 10,000 square meter facility with around 200 skilled workers producing 40,000 acetate frames monthly . Wenzhou G&D Glasses, founded in 1999, produces both metal and acetate optical frames and sunglasses with over 150 staff and annual output of 700,000 pieces . Xiamen, Fujian province is another significant hub with companies like Xiamen Langxue Spectacles, established in 1999, operating nearly 15,000 square meters of workshop space . Shenzhen also hosts manufacturers such as Shenzhen Deepward, founded in 2010 with 80 to 100 workers specializing in handmade acetate eyewear .
Material Selection and Preparation
Quality acetate production begins with careful material selection within the acetate sunglasses factory. Premium manufacturers use acetate from renowned suppliers like Mazzucchelli, an Italian company producing organic acetate consisting primarily of renewable cotton fiber and wood pulp . Raw acetate arrives in large sheets, typically eight millimeters thick for frame fronts and six millimeters for temples . Sheets are cut into manageable strips using circular saws before further processing . Some factories also prepare material by cutting large blocks into smaller pieces and baking them in ovens to remove moisture and increase hardness, ensuring finished frames resist deformation .
CNC Machining and Shaping
Modern acetate sunglasses factory operations rely heavily on computer-controlled machining. Frame fronts are cut from flat acetate sheets using CNC milling machines that follow digital designs with multiple cutting tools achieving required shapes and accuracies . As many as thirty machining stages may be applied to each frame front . The process includes inner circle machining creating lens openings and outer circle profiling defining the frame shape . Temple pieces are also CNC machined separately from slightly thinner acetate sheets . Some factories utilize precision engraving machines programmed with detailed specifications for inner shape, groove depth, and overall geometry .
Lamination and Decoration Techniques
Many acetate frames feature multi-layer colors and patterns created through lamination within the acetate sunglasses factory. Small pieces of colored acetate are cut and拼贴 onto base frames before being permanently bonded . After bonding, frames must rest for at least twelve hours ensuring secure adhesion without future cracking . For frames with decorative metal elements including core wires inside temples, specialized machines drill precise holes and insert metal components . Core wire insertion strengthens temples and maintains shape while allowing adjustment .
Tumble Polishing Process
After machining, acetate parts have sharp edges and cutting marks requiring smoothing through tumble polishing . Motorized octagonal wooden drums contain twenty to thirty kilograms of small beech wood polishing pegs mixed with abrasive compounds . Frames and media seal inside drums rotating continuously for twenty-four hours per stage . Most factories use multiple stages with progressively finer media, often four phases from rough to fine polish taking four consecutive days total . This process removes machining marks and creates smooth surfaces ready for final finishing . Some factories invest heavily in tumbling technology, with Deepward operating forty tumblers after investing over one hundred fifty thousand dollars in research and development .
Hand Polishing and Finishing
Hand polishing represents a critical skilled craft within any acetate sunglasses factory. After tumbling, frames are hand polished using four increasingly finer grades of wax compounds applied with various width polishing mops . Every surface including the bridge aperture receives meticulous attention to achieve consistent lustrous gloss . Hand polishing requires good feel and experience, as too much pressure can burn acetate through friction while insufficient pressure leaves imperfections .
Core Product Definition
A digital air flow sensor is an advanced measurement device that quantifies the mass or volume of air moving through a system and outputs the data as a digital signal rather than a variable analog voltage. These sensors combine microelectromechanical systems technology with onboard application-specific integrated circuits that perform signal processing, temperature compensation, and calibration directly within the sensor housing. The result is a precision component that delivers clean, interference-resistant data to engine control units, industrial controllers, or medical devices with minimal signal conditioning required.
Fundamental Operating Principles
Most digital air flow sensors operate on the heat transfer principle, where a thermally isolated heating element and temperature sensing resistors measure how airflow carries heat away from the heated surface . A microbridge MEMS structure with thin-film platinum and silicon nitride resistors maintains precise temperature control . As air flows past the sensing element, the cooling effect requires more electrical current to maintain target temperature, and this current draw directly correlates to air mass passing through the sensor. The integrated ASIC converts this analog relationship to a calibrated digital output, typically through I²C communication protocols, with response times as fast as one millisecond .
Hot Wire and Hot Film Technologies
Modern digital air flow sensors utilize either hot wire or hot film sensing elements. Hot wire designs use a thin platinum wire suspended in the air stream that responds rapidly to flow changes but may be more susceptible to contamination. Hot film sensors deposit the sensing element on a ceramic or silicon substrate, creating a more durable surface that withstands particle impingement while maintaining excellent sensitivity . Both technologies benefit from digital processing that compensates for ambient temperature variations and sensor aging, maintaining accuracy across operating ranges from minus forty degrees to over one hundred twenty degrees Celsius.
Karman Vortex Digital Sensors
An alternative approach to digital air flow sensing uses Karman vortex principles rather than thermal measurement. These sensors place a vortex generator in the air stream that creates alternating vortices with shedding frequency directly proportional to air velocity . Optical or ultrasonic detectors capture the vortex frequency and convert it to a digital square wave signal. Toyota has employed this technology extensively, with sensors outputting five-volt square waves where frequency varies from approximately thirty hertz at idle to over one hundred sixty hertz at wide-open throttle . This method offers exceptional durability since sensing elements never contact the air stream directly.
MEMS Technology Integration
Microelectromechanical systems form the heart of modern digital air flow sensor design. Silicon micromachining creates microscopic bridges and channels with precise geometries that ensure repeatable flow characteristics . Temperature-sensitive resistors deposited with thin-film techniques achieve tolerances impossible with conventional manufacturing. The tiny thermal mass of MEMS structures enables response times measured in milliseconds, capturing rapid transients that affect system performance. Multiple sensing elements on a single chip can measure flow direction, temperature differentials, and backflow events simultaneously.
Onboard Signal Processing
The defining feature of a digital air flow sensor is its integrated signal processing capability. Rather than outputting raw analog voltages that require external conditioning, these sensors contain ASICs that linearize the sensing element response, apply temperature compensation algorithms, and calibrate output to engineering units . The digital output eliminates susceptibility to electrical noise that plagues analog signals in electrically harsh environments like engine compartments or industrial facilities. Twelve to sixteen-bit resolution provides fine granularity, detecting flow changes as small as 0.05 percent of full scale .
Digital Communication Protocols
Digital air flow sensors communicate through standardized protocols that simplify system integration. I²C interfaces are common for medical and industrial applications, allowing multiple sensors to share the same two-wire bus with individual addressing . Frequency output formats suit automotive applications where engine control units have dedicated input capture timers. Some sensors offer configurable outputs that can be programmed for specific system requirements. The digital nature of these signals means cable length and routing have minimal impact on measurement integrity.
Core Business Definition
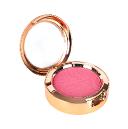
Baked blusher manufacturers are specialized cosmetic production companies that formulate and produce blushers using a unique baking process that involves heating liquid or cream-based formulas to create silky, dome-shaped powder products. Unlike traditional pressed powders that are simply compacted, baked blushers undergo controlled thermal processing that fuses pigments, binders, and pearlescent minerals together, resulting in enhanced luminosity, smoother blendability, and buildable color intensity. These manufacturers serve global beauty brands, private label companies, and retailers seeking to offer consumers the distinctive natural glow effect that baked textures deliver.
Manufacturing Facilities and Global Presence
Major baked blusher manufacturers operate substantial production facilities equipped with specialized baking technology. Industry leaders like Cosmax, founded in South Korea in 1992, operate across Asia, the United States, and beyond, serving both global giants and mid-sized beauty brands with substantial research and development investment. Intercos, established in Italy in 1972 with over fifty years of cosmetic manufacturing experience, operates in Europe, Asia, and North America, producing baked blushers for top global brands. TY Cosmetic, founded in 2009 in Guangzhou, China, runs three manufacturing plants serving over one thousand global clients with a focus on startup and growing brand support. Lady Burd, a family-owned American manufacturer based in New York operating since 1968, provides personal private label services for salons, spas, and indie brands.
The Baking Process Technology
The heart of production lies in the unique baking process that distinguishes these products from conventional blushers within baked blusher manufacturers facilities. Liquid or cream-based cosmetic paste containing pigments, binders, and pearlescent agents is poured into concave bases, often made from porous materials like terracotta that allow moisture evaporation during baking. The filled bases are placed in ovens at atmospheric pressure with precise temperature control, typically ranging between thirty and eighty degrees Celsius, for periods ranging from eight to twenty-four hours. This slow baking evaporates the volatile components until moisture content falls below one percent, transforming the liquid mixture into solid yet silky powder blocks with characteristic dome-shaped surfaces and enhanced luminous properties.
Raw Material Selection and Quality
Ingredient quality determines final product excellence within baked blusher manufacturers operations. High-purity mica provides luminous reflection and forms the structural foundation of baked formulations. Iron oxides and organic pigments deliver vibrant yet wearable shades in various color ranges. Talc or talc alternatives create the base texture while skin-conditioning agents improve comfort and adhesion. Manufacturers carefully evaluate suppliers and perform strict incoming inspections including heavy metal screening, microbiological analysis, and ingredient stability testing before materials enter production lines. This attention to raw materials protects consumers and strengthens brand credibility in competitive international markets.
Temperature Precision and Control
Temperature control represents critical technology within baked blusher manufacturers engineering. Excessive heat during baking can dull pigmentation and compromise color vibrancy, while insufficient baking may weaken structural integrity causing breakage during shipping or use. Modern facilities use programmable ovens with digital temperature monitoring to maintain uniform heating cycles across all production batches. After baking, cooling phases must be carefully managed to prevent cracking or surface irregularities that would render products unsellable. Automated dust removal systems ensure smooth finishes before packaging. Consistency in baking time and environmental control ensures every batch meets identical shade and texture standards.
Formula Development and Customization
Creating new baked blusher formulations requires specialized expertise within baked blusher manufacturers research and development teams. Matte finishes require different pigment and binder ratios compared to shimmer or metallic varieties that incorporate higher pearl concentrations. Skin feel optimization balances powder smoothness against adhesion and wear characteristics. Color matching involves blending multiple pigments to achieve precise shade targets specified by brand customers. Stability testing ensures formulations maintain appearance and performance through temperature variations encountered during shipping and extended shelf life. Preservative efficacy testing confirms microbial safety throughout product life.
Core Business Definition
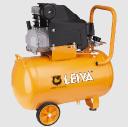
An air compressor machine factory specializes in manufacturing equipment that converts power into potential energy stored in pressurized air. These facilities produce a wide range of compressors including reciprocating piston types, rotary screw models, and centrifugal units for diverse industrial applications. The manufacturing process combines precision machining, assembly operations, and rigorous testing to create reliable machines serving automotive workshops, food processing plants, pharmaceutical facilities, and large-scale manufacturing operations worldwide.
Compressor Types and Technologies
Several distinct compressor technologies emerge from an air compressor machine factory production lines. Reciprocating compressors use pistons driven by crankshafts to compress air in cylinders, ideal for applications requiring high pressure in intermittent duty cycles. Rotary screw compressors employ meshing helical rotors to provide continuous airflow for steady industrial operations. Centrifugal compressors utilize high-speed impellers for large-volume applications in power generation and chemical processing. Each type requires specialized manufacturing equipment and assembly techniques tailored to its operating principles.
Manufacturing Processes Overview
Production within an air compressor machine factory involves multiple sophisticated operations. Component manufacturing includes casting of housings, machining of cylinders and rotors, and fabrication of pressure vessels. Assembly lines integrate motors, compression elements, cooling systems, and control panels into complete packages. Testing stations verify performance parameters including flow rates, pressure capabilities, and power consumption. Quality control throughout ensures each compressor meets design specifications before shipment.
Reciprocating Compressor Production
Manufacturing piston compressors requires precision machining of cylinders and crankshafts within the air compressor machine factory. CNC lathes create cylinder bores with exacting tolerances ensuring proper piston fit and compression efficiency. Valve seat grinding machines produce sealing surfaces critical for preventing backflow during operation. Piston ring installation requires careful assembly to maintain compression while minimizing friction. Connecting rods and crankshafts undergo balancing to reduce vibration during high-speed operation.
Rotary Screw Manufacturing
Screw compressor production demands advanced machining capabilities within the air compressor machine factory. Five-axis CNC machining centers profile rotors with complex helical geometries requiring micron-level precision. Rotor grinding machines achieve surface finishes essential for efficient meshing without contact. Housing machining creates precise bore alignments maintaining clearances measured in thousandths of millimeter. Gear and bearing installation systems ensure smooth synchronization of male and female rotors during operation.
Centrifugal Compressor Fabrication
Large centrifugal compressors require specialized production techniques in the air compressor machine factory. Impeller machining from solid forgings creates complex blade geometries using five-axis milling operations. Dynamic balancing machines verify rotating assemblies operate without vibration at high speeds. Diffuser and volute castings require precision machining to maintain aerodynamic efficiency. Assembly in clean environments prevents contamination affecting high-speed operation.
Pressure Vessel Manufacturing
Air receivers and separator tanks represent critical components produced within air compressor machine factory operations. Plate rolling forms cylindrical shells from steel sheets of specified thickness. Automated welding creates seams meeting pressure vessel code requirements. Nozzle attachment provides connections for inlet, outlet, and safety devices. Hydrostatic testing verifies vessels withstand rated pressures without leakage. Surface preparation and painting protect against corrosion throughout service life.
Electric Motor and Drive Integration
Compressor drive systems require careful integration within air compressor machine factory assembly. Motor mounting maintains alignment with compressor shafts preventing coupling wear. Belt drive installation requires proper tensioning for efficient power transmission. Direct coupled systems use flexible couplings accommodating minor misalignment. Variable frequency drives enable speed control matching output to demand. Starter and control wiring connects motors to power sources and safety systems.
Core Business Definition
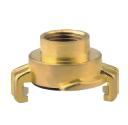
Quick joint manufacturing refers to the production of specialized fittings that enable rapid connection and disconnection of fluid lines without tools. These components, also called push-to-connect fittings, instant fittings, or quick-connect couplings, create secure seals through internal gripping mechanisms that lock tubing or pipe upon insertion. Manufacturers produce these products for pneumatic systems, hydraulic applications, water treatment, medical equipment, and industrial fluid transfer where installation speed and maintenance access drive design requirements. The global market encompasses brass, stainless steel, plastic, and composite variants serving diverse pressure and compatibility needs.
Product Categories and Types
Several distinct product lines emerge from quick joint manufacturing operations. One-touch fittings feature collet gripping mechanisms releasing tubing when the collet is pressed. Push-to-connect fittings automatically lock tubing upon insertion requiring no additional action. Quick-couplers consist of male and female halves joining with a single motion. Multi-port connectors combine several connections in single bodies for complex installations. Rotary unions enable fluid transfer between stationary and rotating equipment. Each type serves specific application requirements across industries.
Operating Principles
Quick joints function through precision-engineered internal components within quick joint manufacturing designs. A gripping collet with angled teeth captures tubing inserted into the fitting, preventing withdrawal under pressure. An O-ring or seal compresses against tubing outer diameter creating leak-free sealing. A release mechanism, typically a push sleeve or button, deflects collet teeth allowing tubing removal. Body materials provide structural integrity containing system pressure. This elegant mechanism enables tool-free installation while maintaining reliable performance through thousands of connection cycles.
Materials Selection
Material choice fundamentally affects quick joint performance and application suitability. Brass fittings dominate general industrial and pneumatic applications offering good strength, corrosion resistance, and cost effectiveness. Stainless steel variants serve food processing, pharmaceutical, and corrosive chemical environments requiring enhanced compatibility. Engineering plastics including acetal, nylon, and PEEK provide lightweight, non-corrosive options for specific applications. Composite materials combine properties of multiple constituents for optimized performance. Material expertise distinguishes qualified quick joint manufacturing operations serving demanding industries.
Machining Operations
Precision machining forms the foundation of quick joint manufacturing for metal components. CNC turning centers shape brass or stainless steel bar stock to exacting dimensional specifications. Multi-axis machining creates complex internal features including seal grooves, thread forms, and collet retention details. Surface finishing operations remove machining burrs ensuring smooth operation and seal compatibility. Thread cutting or rolling produces accurate thread forms meeting international standards including BSP, NPT, and metric configurations. Automated inspection verifies critical dimensions before assembly.
Injection Molding for Plastic Components
Plastic quick joints require specialized injection molding capabilities within quick joint manufacturing facilities. Precision molds produce complex body geometries with smooth internal surfaces essential for seal performance. Material selection includes glass-filled formulations for enhanced strength and dimensional stability. Gate location design ensures complete cavity filling without voids or weld lines. Cooling channel optimization controls cycle times while maintaining dimensional accuracy. Multi-cavity tooling maximizes production efficiency for high-volume requirements.
Seal Manufacturing and Integration
Reliable sealing depends on precision elastomeric components within quick joint manufacturing assembly. O-rings molded from NBR, EPDM, FKM, or other compounds provide primary sealing between fitting and tubing. Backup rings prevent seal extrusion under high pressure. Wiper seals exclude contaminants from internal mechanisms. Seal material selection considers fluid compatibility, temperature range, and wear requirements. Automated assembly equipment installs seals consistently at production speeds.
Core Business Definition
A duck toy factory specializes in manufacturing playful duck-shaped products for children's entertainment and educational purposes. These facilities produce everything from simple rubber bath ducks to complex plush dolls, pull-along wooden toys, and interactive electronic duck toys with sound and movement capabilities. The category spans multiple materials, including vinyl, plastic, fabric, and wood, depending on target age groups and play environments. Manufacturers serve retail chains, specialty toy stores, promotional product distributors, and direct-to-consumer channels worldwide.
Popular Duck Toy Varieties
Several distinct duck toy types emerge from production lines in a typical duck toy factory. Classic rubber bath ducks remain perennial favorites with simple squeeze mechanisms producing squeaking sounds during water play. Plush duck dolls with soft fabric bodies appeal to younger children seeking comfort and cuddle companions. Pull-along wooden ducks with rolling wheels entertain toddlers developing motor skills through walking play. Electronic duck toys with programmed movements and songs engage older children through interactive features. Educational duck toys teach colors, numbers, or animal sounds through playful interaction.
Materials and Safety Standards
Child safety drives every material selection within a responsible duck toy factory. Phthalate-free vinyl ensures bath toys remain safe despite repeated mouth contact during water play. Food-grade silicone provides an alternative material for teething ducks used by infants. BPA-free plastics prevent chemical exposure concerns among health-conscious parents. Non-toxic paints and dyes maintain color appeal without heavy metal content. Flame-retardant fabrics meet sleep safety requirements for plush toys intended for nursery use. Compliance with international standards, including ASTM F963 and EN71, remains essential for global distribution.
Manufacturing Processes
Production within a duck toy factory employs multiple fabrication techniques matched to product types. Rotational molding creates hollow vinyl bath ducks with seamless construction and consistent wall thickness. Injection molding produces rigid plastic components for electronic toy housings and pull-along wheels. Sewing and stuffing operations transform fabric cut pieces into plush duck dolls with controlled softness. Electronic assembly integrates circuit boards, speakers, and sensors into interactive toy bodies. Painting and decorating stations apply facial features and patterns, completing visual appeal.
Mold Making and Tooling
Creating duck-shaped products begins with precision mold fabrication within or for the duck toy factory. Skilled toolmakers machine steel or aluminum molds with cavity shapes matching desired duck contours. Surface finishing determines final product texture from smooth glossy to soft matte appearances. Multi-part mold designs accommodate undercuts like beaks and wings, requiring complex ejection systems. Sample molding validates tooling accuracy before production commitment. Mold maintenance programs preserve dimensional accuracy across millions of production cycles.
Quality Control Systems
Consistent product quality depends on rigorous inspection throughout the duck toy factory operations. Incoming material testing verifies plastic compounds meet specifications before production use. In-process checks monitor molding parameters, ensuring consistent part formation. Functional testing confirms squeakers produce sound and electronic features operate correctly. Pull testing validates the secure attachment of eyes, beaks, and other small components. Finished product sampling simulates use conditions, verifying durability before shipment.
Design and Development
New duck toy concepts originate through collaboration between designers and duck toy factory engineers. Sketch concepts evolve into 3D computer models defining exact proportions and features. Prototype fabrication tests design feasibility and gathers consumer feedback. Material selection balances cost targets against durability and safety requirements. Packaging design protects products while communicating appeal at retail. Development timelines coordinate all activities from concept to production readiness.
Seasonal Production Planning
Duck toy factory operations must align with seasonal demand patterns affecting the toy industry. Spring production builds inventory for summer bath toy sales peaks. The summer months focus on back-to-school and holiday season preparation. Fall represents peak production for fourth-quarter retail delivery. Winter allows maintenance periods and new product development. Accurate forecasting prevents shortages during demand spikes while avoiding excess inventory carrying costs.